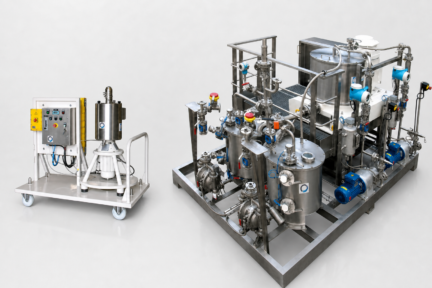
Centrifuges & Centrifugal Extractors for R&D through Production Capacities
Partners In Process Development!
Rousselet-Robatel is your partner in process development. We are focused on delivering improvements within research labs and production facilities, and together with our clients, we transform the ordinary into the extraordinary.
- Rare Earth Element Extraction by Hydrometallurgy
- Scale-Up Centrifugation for API Pharmaceutical Development & Production
- Gentle Recovery of Sensitive Biologic Materials using Sold Bowl Decanters
- Centrifugation Technologies for Recycling & Reuse Treatment Lines
- Modern Extraction Technologies in Nuclear Fuel Cycle Applications
- Safely Concentrate PFAS Contaminated Process Streams using the Model LX Pfastractor™
- Purification of Complex Molecular Species using Kromaton FCPC® Chromatography
- Isolate and Recover Pharmaceutical Grade Cannabinoids using Cannafuge® Technologies
- Textile
- Metalworking/Deoiling of Machined Parts
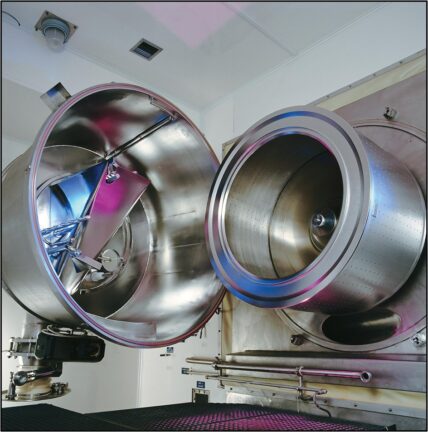
Model EHBL Horizontal Axis Peeler Centrifuge
Partners In Process Development
Rousselet-Robatel is your partner in process development. We are focused on delivering improvements within research labs and production facilities, and together with our clients, we transform the ordinary into the extraordinary.
- Rare Earth Element Extraction by Hydrometallurgy
- Scale-Up Centrifugation for API Pharmaceutical Development & Production
- Gentle Recovery of Sensitive Biologic Materials using Sold Bowl Decanters
- Centrifugation Technologies for Recycling & Reuse Treatment Lines
- Modern Extraction Technologies in Nuclear Fuel Cycle Applications
- Safely Concentrate PFAS Contaminated Process Streams using the Model LX Pfastractor™
- Purification of Complex Molecular Species using Kromaton FCPC® Chromatography
- Isolate and Recover Pharmaceutical Grade Cannabinoids using Cannafuge® Technologies
- Textile
- Metalworking/Deoiling of Machined Parts
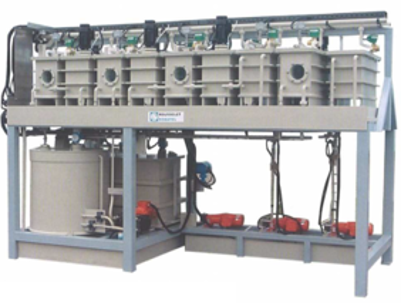
Mixer Settler for Hydrometallurgy
Rare Earth Element Extraction by Hydrometallurgy
Engineering Challenge: Purification and Efficient Recovery REE’s
Processing purified REEs such as Yttrium, Cerium, Neodymium, Europium, Terbium, and Dysprosium into high purity, commercially viable products ready for use in critical modern engineered electronic systems such as batteries, lights, hard drives, hybrid vehicles, and guidance systems.
Hydrometallurgical solvent extraction is the most critical and difficult stage of rare earth refining where effective extraction requires precise control of phase chemistry (pH, density ratios, concentrations, temperatures).
Process Technology Solution: Hydrometallurgical Extraction
Hydrometallurgical extraction is known as the preferred method for efficiently extracting these rare earth elements, which are known for their superconductivity, ferro-magnetism, and brightness. These properties are only achieved when elemental purity is accurately controlled.
In this modular, staged extraction architecture, Rousselet-Robatel mixer-settlers achieve 99.5 – 99.9% purity for REEs such as Nd, Dy, or Tb, which is the result of many cumulative mechanical extraction stages where high stage efficiency from stage to stage leads to improved purification levels.
It is this disciplined execution of complex, high-precision extraction processes where the mechanical stability of the system and its hydraulic control operate seamlessly together.
Competitive Advantages: Compatible, Sustainable, Proven
- Compatible: Equipment integrates into existing hydrometallurgy flow sheets.
- Sustainable: Lower energy consumption, decreased pollutant rates, and reduced emissions.
- Proven: Clients receive the benefit of Rousselet-Robatel’s long history and extensive process knowledge that reduces operational risks and maintenance uncertainties while delivering exceptional chemical purity.
Model EHBL Horizontal Axis Peeler Centrifuge
Scale-Up Centrifugation for API Pharmaceutical Development & Production
Engineering Challenge: Preserve Product Purity and Yield at Scale
Industrial scale-up can introduce new impurities—or increase existing ones—relative to lab and pilot processes. Flexible suites must handle varied products while consistently delivering on-spec API by linking critical process parameters to quality attributes.
Process Technology Solution: cGMP Horizontal Axis Peeler Centrifuge
The purity and quality of the active pharmaceutical ingredient (API) are critical determinants of both therapeutic performance and patient safety. To support these requirements within a highly regulated pharmaceutical manufacturing environment, Rousselet-Robatel applies advanced process analytical technologies (PAT), process intensification principles, and application-specific automation and control strategies to optimize unit operation performance.
The resulting process solutions provide the flexibility to scale production capacity up or down while maintaining rigorous product quality standards and regulatory compliance. The integration of these technologies can substantially reduce equipment footprint, lower energy demand, enhance process control, and deliver significant improvements in manufacturing productivity, efficiency, and cost effectiveness.
Competitive Advantages: Consistent, Fast Implementation, Proven Performance
- Consistent: Producing results where conventional systems can struggle. RR equipment maintains stable output as feed-stream flow changes, giving customers a decisive advantage in product quality, throughput, and process reliability.
- Fast Implementation: Without sacrificing flexibility, these modular, skid-mounted systems integrate into new or existing facilities with less disruption—shortening time to operation, simplifying expansion, and reducing project risk.
- Performance: From day one, RR treatment systems reduce compliance and performance risks. Decades of field-proven experience, fabrication to cGMP and GAMP requirements, and alignment with CE, ISO, and UL standards provide an audit-ready solution that less-established alternatives cannot easily match.
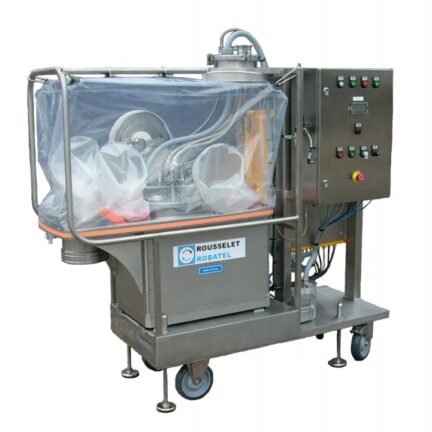
Decanter Centrifuge with Soft-sided Barrier Isolation
Gentle Recovery of Sensitive Biologic Materials using Sold Bowl Decanters
Engineering Challenge: High Solids Loading & Shear Sensitivity
As upstream bioprocessing continues to drive higher cell densities and product titers, clarification of high-solids process streams has become a critical separation challenge. Feed streams containing more than 20% solids by volume require robust clarification technologies capable of maintaining throughput, separation efficiency, and process stability under demanding operating conditions.
Equally important is the preservation of cell viability during clarification, as excessive shear forces within the feed path can induce cell rupture and the release of intracellular contaminants, impairing clarification performance and increasing downstream purification demands. Consequently, effective clarification systems must combine high solids-handling capability with low-shear processing to preserve cell integrity and ensure consistent process performance.
Process Technology Solution: Solid Bowl Decanter Centrifuges
For specialized biologic materials derived from a variety of host cells, decanter centrifuges are used in operations including whole-cell recovery, post-lysis clarification, and product isolation. Rousselet-Robatel solid-bowl decanter centrifuges provide low-shear feed handling and gentle solids recovery, even at feed concentrations exceeding 20% by volume. As washing and concentration stages progressively enhance pellet purity, these systems support continuous, enclosed processing with automated solids discharge triggered by either predefined cycle times or turbidity-based process control.
Competitive Advantages: Compatible, Flexible, Proven
- Broad Compatibility: Proven across a wide range of biologic processes, solid-bowl decanters are compatible with mammalian, bacterial, fungal, and other host-cell systems, enabling a common platform for diverse production requirements.
- Flexible Integration: Modular, skid-mounted designs simplify implementation in both greenfield and brownfield facilities, reducing installation complexity, accelerating project timelines, and supporting future process expansion.
- Proven Reliability: Backed by extensive operating experience in bioprocessing applications, Rousselet-Robatel decanters are manufactured in accordance with cGMP requirements and international CE standards, providing confidence in regulatory compliance, operational performance, and long-term asset reliability.
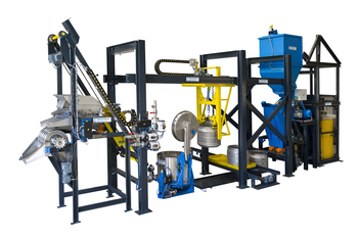
Recycling/Reuse Treatment Line with Filtering Centrifuge
Centrifugation Technologies for Recycling & Reuse Treatment Lines
Engineering Challenge: Volume of Waste & Economic Viability
Despite ongoing efforts to improve material recovery rates, the generation of electronic, plastic, and industrial waste continues to outpace the capacity of existing recycling infrastructure. As waste volumes increase, recycling technologies must deliver higher throughput, improved recovery efficiency, and greater operational reliability to remain effective at scale.
The success of recycling operations depends on balancing environmental benefits with economic performance. The value recovered from recycled materials must justify capital investment in processing systems and infrastructure while supporting sustainable operating costs and long-term profitability.
Process Technology Solution: Continuously Operating Recycling/Reuse Treatment Lines
Continuous processing systems for the separation, cleaning, and drying of materials generated by machining, metalworking, and plastics manufacturing operations can significantly reduce processing time, labor requirements, and operating costs. By integrating application-specific centrifuge technologies with advanced automation and robotic handling,
Rousselet-Robatel delivers higher separation efficiency, improved product quality, and greater process consistency. This integrated approach streamlines material recovery and recycling operations, enabling more sustainable resource utilization while enhancing overall plant productivity and economics.
Competitive Advantages: Yield, Efficiency, Versatility
Rousselet-Robatel centrifuge systems deliver a strong return on investment by maximizing material recovery, reducing operating costs, and supporting sustainability objectives.
- Yield: High recovery yields produce recycled materials with quality and consistency comparable to virgin feedstocks, even in high-volume applications.
- Efficiency: Improvements in energy efficiency, waste diversion, and emissions reduction enhance environmental performance and support regulatory and corporate sustainability goals.
- Versatility: Proven across a wide range of industrial recycling processes, specialty centrifuges generate measurable economic benefits throughout the treatment line, improving the efficiency of material cleaning, dewatering, drying, and recovery operations while increasing the value of recovered products.
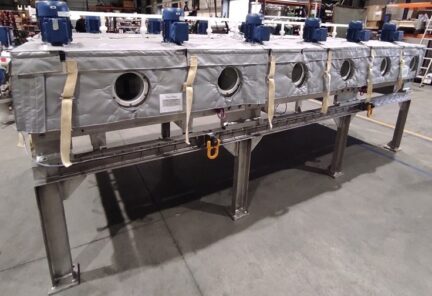
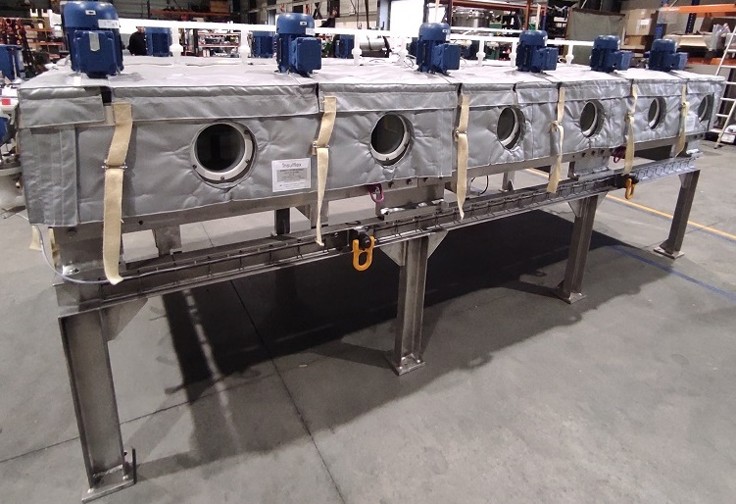
Mixer-Settler for Nuclear Fuel Processing (shown with insulation)
Modern Extraction Technologies in Nuclear Fuel Cycle Applications
Engineering Challenge: Solvent Degradation, Corrosion, Radioactive Waste Management
PUREX (Plutonium Uranium Redox EXtraction) processing presents several key chemical and operational challenges during spent nuclear fuel reprocessing, which together increase process complexity, operating costs, equipment maintenance requirements, and overall plant safety considerations.
- Solvent degradation: Tributyl phosphate (TBP) degrades under radiation, elevated temperatures, and nitric acid exposure, producing byproducts such as dibutyl phosphate that can impair separation performance.
- Third-phase formation: Solvent degradation products and high metal loadings can cause phase instability, leading to emulsion formation and reduced extraction efficiency.
- Corrosion: Concentrated nitric acid and radioactive process conditions accelerate corrosion of process equipment, increasing maintenance demands.
- Fission product carryover: Difficult-to-separate fission products, including zirconium and technetium, require additional scrubbing and purification steps to achieve product specifications.
- Radioactive waste generation: The process produces significant volumes of high-level liquid waste that must be treated, concentrated, and immobilized for long-term disposal.
Process Technology Solutions: Mixer-Settlers, Centrifugal Contactors
Mixer-settlers and centrifugal extractors are considered standard equipment in the PUREX process because they provide high separation efficiency, excellent phase disengagement, and robust operation in highly radioactive environments.
For mixer-settlers, high stage efficiency enables effective recovery and purification of actinides while removing fission products. Additionally, mixer-settlers are mechanically simple, tolerant of suspended solids and process upsets, and well suited for remote operation and maintenance in nuclear facilities.
The use of centrifugal contactors significantly accelerates the separation of the aqueous and organic phases. This centrifugal force enables short residence times, high stage efficiencies, and reduced solvent hold-up inventories. The compact design minimizes footprint, facilitates rapid start-up and shutdown, and reduces waste volumes associated with flushing and decontamination.
Competitive Advantages: High Stage Efficiency, Excellent Phase Separation, Ease of Scale-Up
While both systems share characteristics such as extraction efficiency, excellent phase separation, mechanical simplicity, and strong tolerance to solids and process upsets, centrifugal contactor technology ensures a lower hold-up relative to throughput, reduced footprint, and faster processing dynamics.
- High Stage Efficiency: Excellent fission product removal, high actinide recovery, and predictable process performance.
- Excellent Phase Mixing and Separation: The PUREX process relies on achieving intimate contact between the aqueous and organic phases and a complete disengagement of phases prior to moving onto subsequent stages.
- Ease of Scale-Up/Scale-Down: PUREX processing plants often process varying quantities of spent fuel. Due to the turn-down capabilities and modular designs, mixer-settlers and centrifugal contactors are able to operate over a wide range of operating conditions with the addition or reduction of stages as required according to the specific process.
Modern Extraction Technologies_Nuclear Fuel
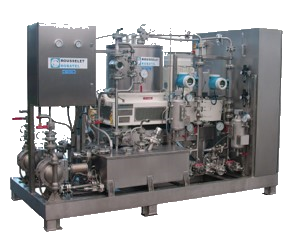
PFASTRACTOR™ Model LX Multistage Centrifugal Extractor
Safely Concentrate PFAS Contaminated Process Streams
Engineering Challenge: High Chemical Mobility, Extremely Stable, Dilute Concentrations
- High Chemical Mobility: PFAS compounds are found in numerous consumer and industrial products, including non-stick cookware, water-repellent clothing, stain-resistant fabrics, and firefighting foams, resulting in extensive opportunities for human and environmental exposure.
- Extremely Stable: PFAS chemicals are resistant to natural degradation and are difficult and costly to remediate requiring energy intensive technologies to destroy its chemical bonds.
- Dilute Concentrations: Treating large volumes of contaminated material having only very dilute concentrations of PFAS drives up the overall costs.
PROCESS TECHNOLOGY SOLUTIONS: Continuous, Multistage Centrifugal Extractors
PFAS contamination presents two major challenges: its widespread use and its persistence in the environment. At the same time, PFAS are notoriously difficult and costly to remove once released with effective remediation typically requiring advanced technologies to destroy the chemical bonds, which can be energy intensive and expensive to implement at scale.
Addressing the PFAS challenge requires an integrated strategy focused on the recovery, recycling, and reuse of valuable fluorinated compounds. The Pfastractor™ Model LX is a continuous liquid-liquid extraction (LLPE) system engineered to recover both long-chain and short-chain perfluorinated substances, including PFAS, PFOS, and PFOA, from contaminated aqueous process streams. Operating in a continuous counter-current configuration, the system efficiently concentrates PFAS compounds into a highly enriched product stream.
The resulting PFAS-rich concentrate is well suited for subsequent remediation, recycling, or reuse, while the treated aqueous phase is substantially depleted of PFAS and can be returned to the process or source stream. By enabling both contaminant removal and resource recovery, the Pfastractor™ supports a more sustainable and circular approach to PFAS management.
Competitive Advantages: Compatible, Sustainable, Proven
- Compatible: Modular, skid-mounted system deployed in the field, and adaptable to existing treatment facilities.
- Sustainable: No requirement for on-site storage silos, no landfill disposal, no incineration of GAC, clay, or other adsorbents.
- Proven: Process volumes from 2 liters per hour for research systems up to 8,000 liters per hour for industrial treatment systems.